Engineered for maximum optical efficiency, severe environment resilience, and DLC/ETL/CE compliance.



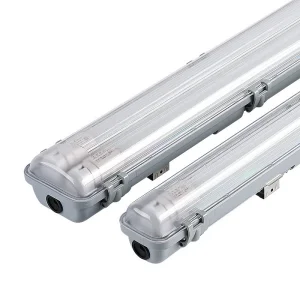
Analyzing macroeconomic drivers, optical performance standards, and ESG integration across heavy industrial sectors.
The global industrial lighting sector is undergoing a profound paradigm shift driven by stringent decarbonization targets, accelerating electricity costs, and rigorous occupational health and safety standards. Commercial and industrial facilities account for over 35% of total building energy consumption worldwide, with legacy Metal Halide (MH), High-Pressure Sodium (HPS), and fluorescent T8 systems representing an enormous source of wasted energy and maintenance overhead.
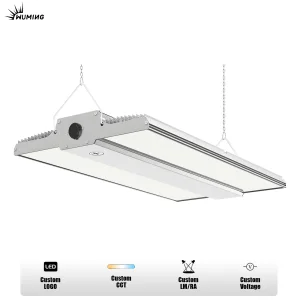
Modern industrial LED fixtures—such as high-efficacy UFO High Bays, Linear High Bays, and Vapor-Tight Tri-Proof lights—deliver optical energy reductions ranging from 60% to 80% over legacy HID installations. Furthermore, when coupled with microwave occupancy sensors and DALI-2 dimming protocols, operational energy savings routinely surpass 85%.
Procuring wholesale LED luminaires from established Chinese manufacturers requires strict adherence to international safety, photobiological, and energy-efficiency certifications. Industrial applications in North America and Western Europe demand compliance with regulatory benchmarks including:
A rigorous examination of semiconductor chipsets, thermal management, optical lensing, and driver topology.
To achieve an operational lifespan exceeding 50,000 hours under continuous 24/7 industrial loads, a professional LED luminaire must balance electrical efficiency with passive thermal dissipation and robust driver protection circuitry.
| Performance Parameter | Standard Commercial Grade | Guangdong Habel Industrial Grade | Engineering Impact / Advantage |
|---|---|---|---|
| Luminous Efficacy | 110 – 130 lm/W | 150 – 190 lm/W | Cuts utility power consumption by up to 35% additional over standard LEDs. |
| LED Chip Architecture | Standard SMD2835 / COB | High-Bin SMD3030 / SMD5050 | Superior thermal tolerance, lower lumen degradation (L70 > 54,000h). |
| Thermal Substrate | Thin Stamped Aluminum Sheet | ADC12 Die-Cast Cold-Forged Aluminum | Junction temp (Tj) kept below 65°C; prevents thermal thermal breakdown. |
| Driver Topology | Non-isolated RC Drivers | Isolated IP67 Mean Well / Inventronics | Resists 6kV–10kV voltage surges, clean power factor (PF > 0.97, THD < 10%). |
| Ingress & Impact | IP20 – IP54 / IK05 | IP65 – IP68 / IK08 – IK10 | Hermetic sealing against dust, steam, chemical vapors, and mechanical impacts. |
| Optical Distribution | Single 120° Wide Lens | 60° / 90° / 120° / Asymmetric Optical Lenses | Delivers targeted foot-candles without spillage glare (UGR < 19 available). |
Heat is the primary cause of LED degradation and driver failure. Industrial high-bay fixtures engineered by Guangdong Habel feature die-cast ADC12 aluminum heatsinks with integrated thermal convection chimneys. This passive air-flow channels heat away from the core LED array, maintaining junction temperatures well within optimal thresholds even in elevated ambient temperatures up to +55°C.
Proper light placement is as critical as total lumen output. Utilizing optical-grade Polycarbonate (PC) and PMMA lenses, our luminaires deliver tailored light patterns—ranging from narrow 60° spot beams for high-racking aisles to asymmetric distributions for perimeter floodlights and stadium high-masts—eliminating dark spots and excessive spill light.
Modern industrial facilities require dynamic adaptive lighting. Our UFO and Linear high bays integrate plug-and-play microwave motion sensors and daylight harvesting sensors. Capable of bi-level dimming (10% standby during inactivity), these smart systems cut operational energy overhead dramatically while supporting continuous asset tracking networks.
Tailored lighting solutions engineered for complex operational environments across global supply chains.
High-bay storage facilities with vertical racking systems exceeding 12 meters present unique lighting challenges. Vertical illuminance, rack surface uniformity, and glare reduction are paramount for forklift operator safety and barcode scanning accuracy.
Solution: Minglight UFO High Bays and Linear LED High Bays (100W–400W) equipped with narrow aisle optics and cold-rated drivers capable of operating continuously at sub-zero temperatures (-40°C) without lumen drop or ignition delay.
Industrial production lines involve exposure to ambient vibration, chemical vapors, airborne dust, and high humidity. Standard fixtures degrade rapidly due to housing corrosion and electrical short circuits.
Solution: Industrial-grade LED Tri-Proof T8 Single/Double Tube Fixtures and explosive-proof canopy lights featuring corrosion-resistant polycarbonate housings, silicone gasket seals, and IK10 impact ratings to guarantee continuous uptime.
Large sports arenas, shipping ports, and railway marshaling yards demand extreme lumen packages with minimal glare, zero flicker (for high-speed camera broadcasting), and wind-resistance engineering.
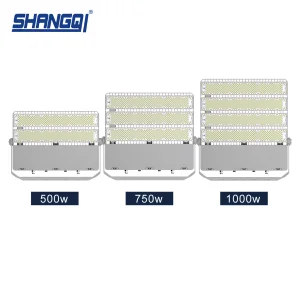
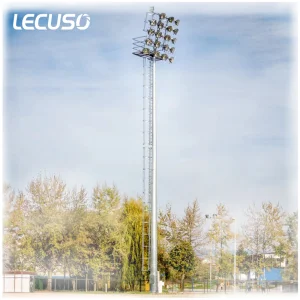
Solution: High-Power LED Module Stadium Lighting (500W to 1000W) combined with octagonal high-mast poles (16m-20m). Features precise multi-angle flood optics, high color rendering (CRI > 80/90), and surge protection up to 20kV.
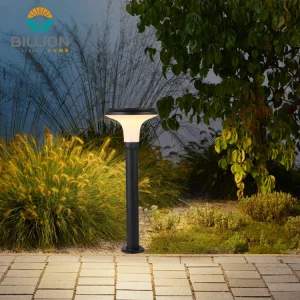
Remote highways, municipal public parks, and perimeter security fences often lack grid power access or require self-sustaining renewable backup lighting systems.
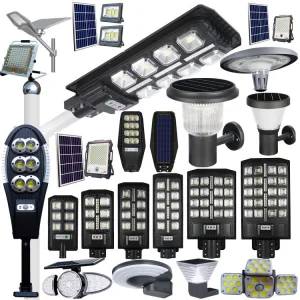
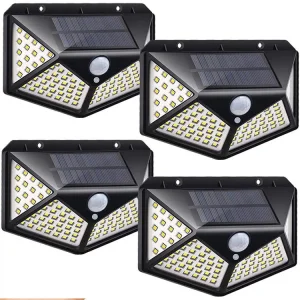
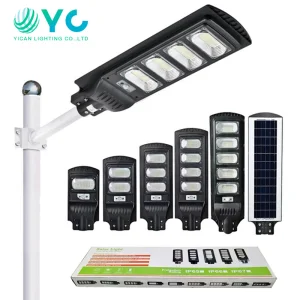
Solution: All-In-One Solar LED Street Lights with high-conversion monocrystalline solar panels, LiFePO4 battery packs, integrated smart PIR motion sensing, and security camera functionality.
Pioneering advancements in smart connected luminaires, semiconductor efficiency, and sustainable manufacturing.
The industrial lighting sector is rapidly evolving from standalone illumination devices into data-gathering IoT nodes. Through wireless mesh protocols like Bluetooth Mesh, Zigbee, and LoRaWAN, luminaires dynamically communicate with building management systems (BMS) to provide occupancy heat maps, asset tracking, and environmental monitoring.
R&D initiatives at Guangdong Habel are targeting system efficacies exceeding 210 lm/W. By leveraging advanced GaN-on-Silicon substrates and nanostructured micro-prismatic optics, future industrial fixtures will reduce energy draw by an additional 25% while maintaining exceptional color fidelity and minimal thermal output.
Future industrial environments prioritize worker circadian rhythms and eco-conscious end-of-life recycling. Modularity will allow individual LED engines, power drivers, and optical lenses to be replaced independently without discarding whole fixtures, promoting zero-landfill industrial operations.
A trusted global manufacturer providing high-grade LED OEM/ODM solutions since 2010.
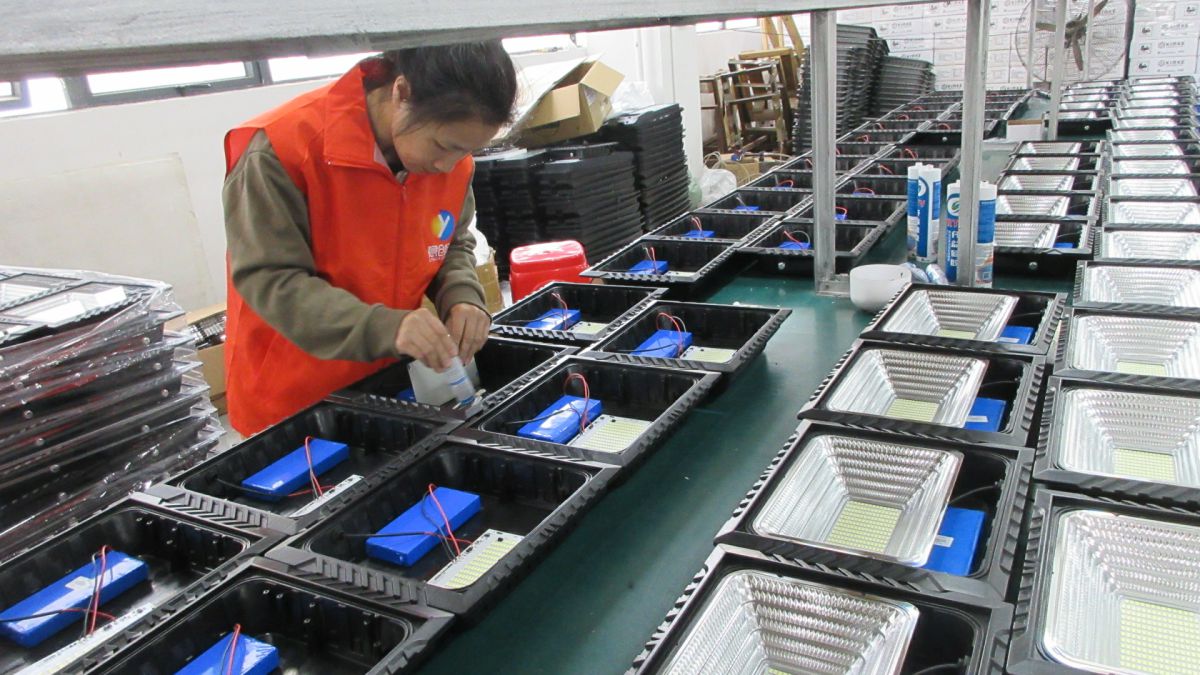
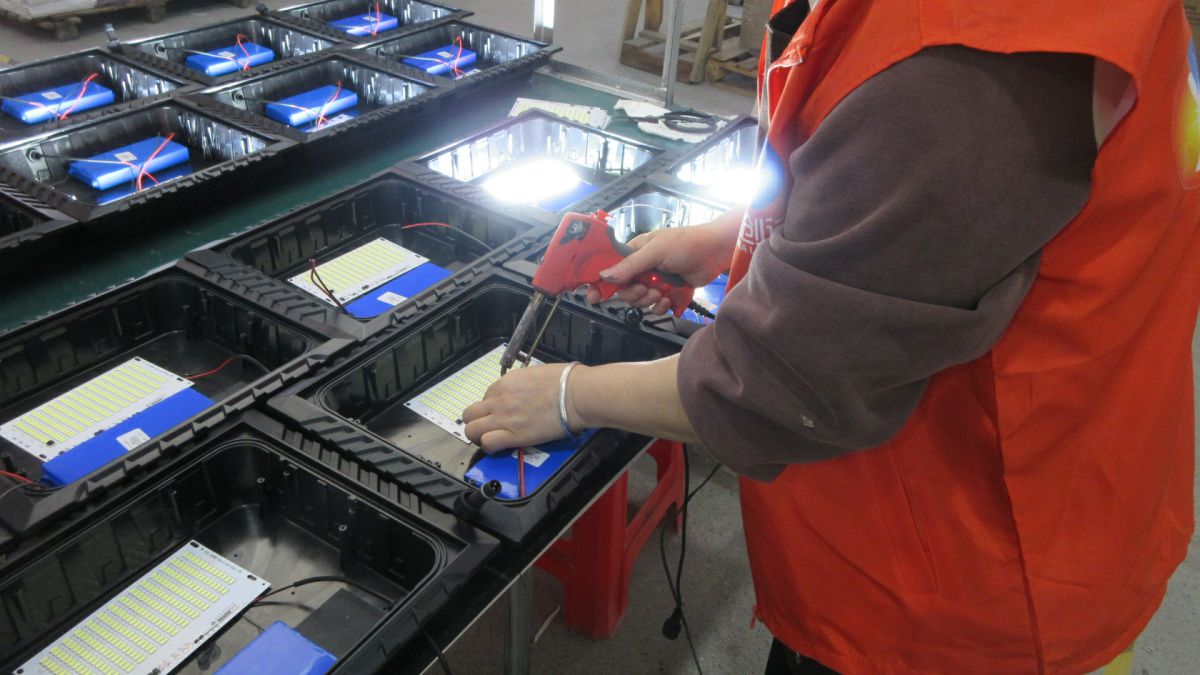
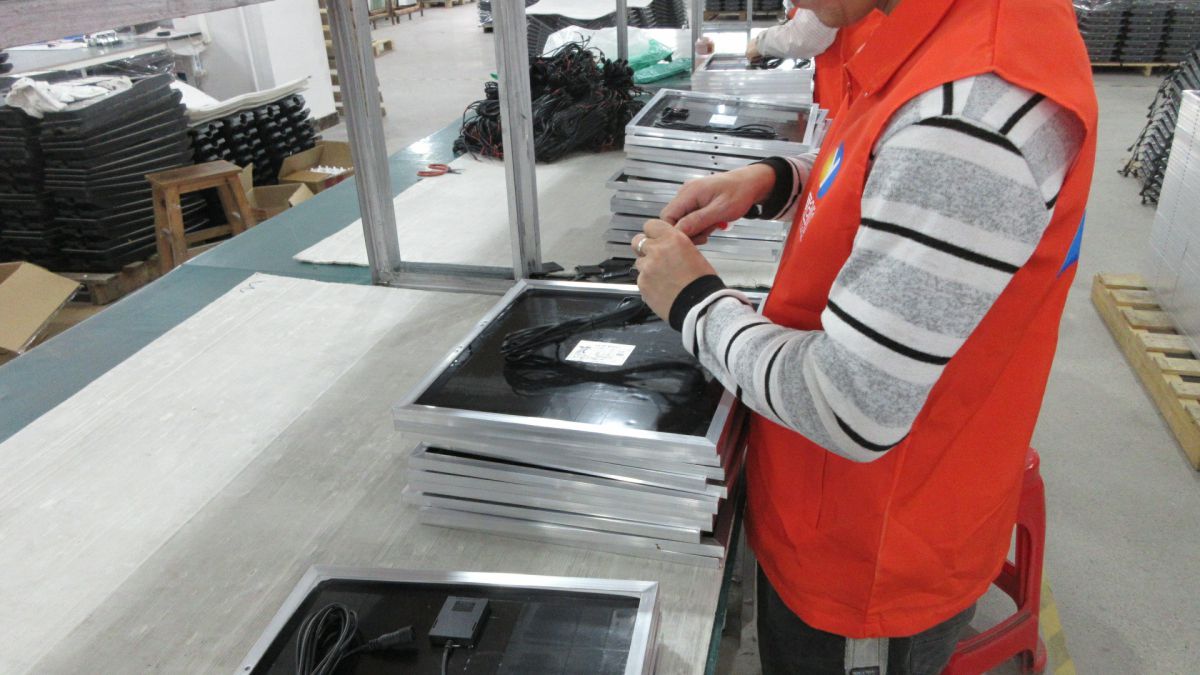
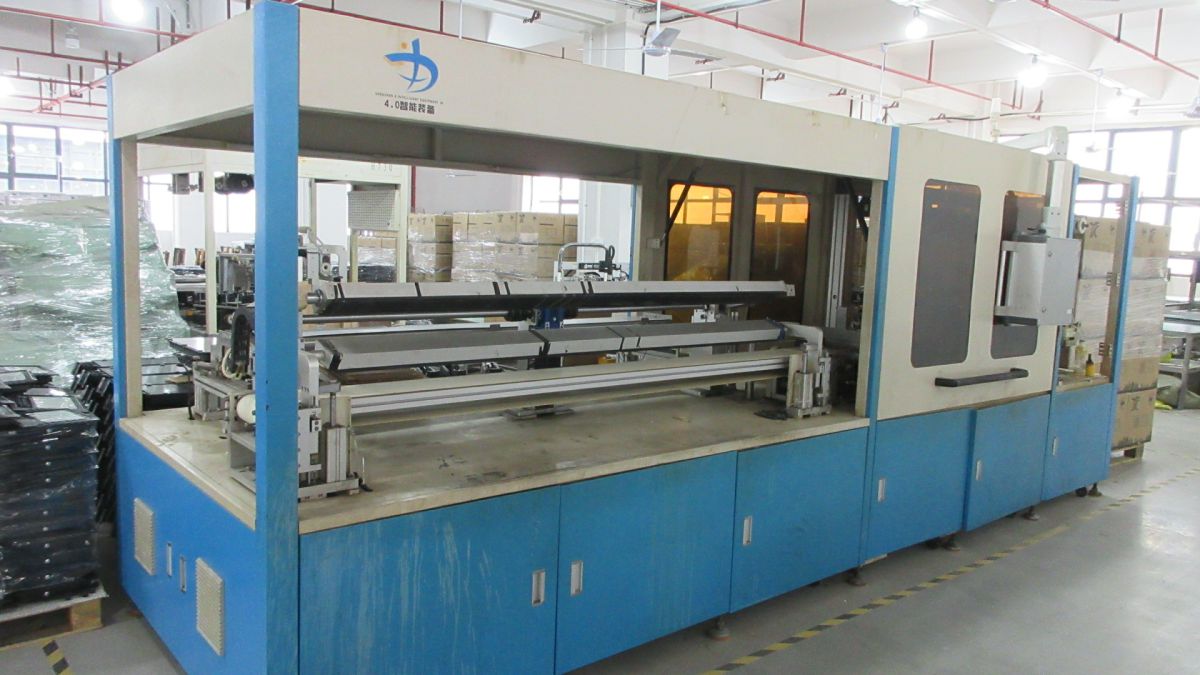
Guangdong Habel Lighting Co., Ltd. was established in 2010. We are a professional manufacturer and exporter specializing in the design, development, and production of LED indoor lighting products and LED outdoor lighting solutions. Over the years, we have built a strong reputation in the lighting industry through continuous innovation, reliable quality, and customer-oriented service.
We are equipped with a powerful R&D team that continuously develops new products every year, ensuring our customers always have access to the latest advancements in lighting technology. By staying at the forefront of LED innovation, we are able to deliver energy-efficient, durable, and high-performance lighting solutions for a wide range of applications. With extensive industry experience and strong technical know-how, Guangdong Habel Lighting has successfully maintained its competitive advantage in the global LED lighting market.
We are committed to building an international lighting brand and actively provide OEM and ODM services to partners worldwide. Our mission is to deliver outstanding lighting solutions that help customers achieve their goals in energy efficiency, sustainability, and cost-effectiveness. We believe in creating long-term partnerships and working together to illuminate a greener and brighter future.
Our leadership team across R&D, quality control, production, and sales departments each has over 5–10 years of experience in the LED lighting industry. This allows us to respond quickly with professional and effective lighting solutions tailored to different market needs.
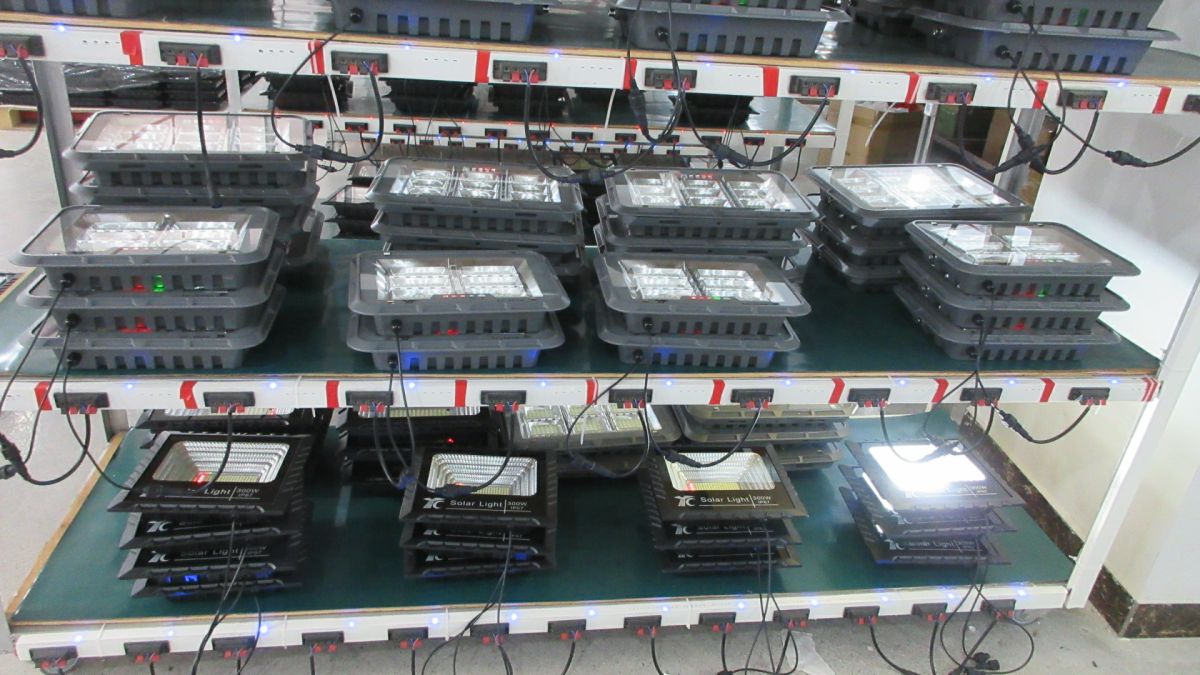
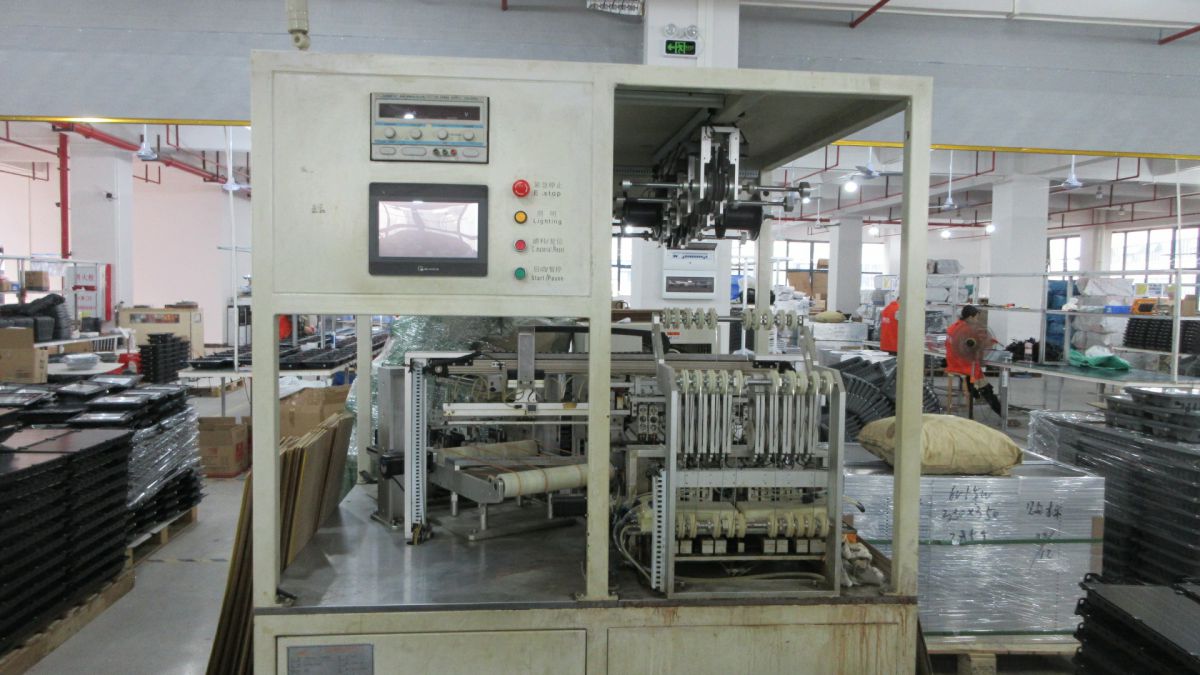
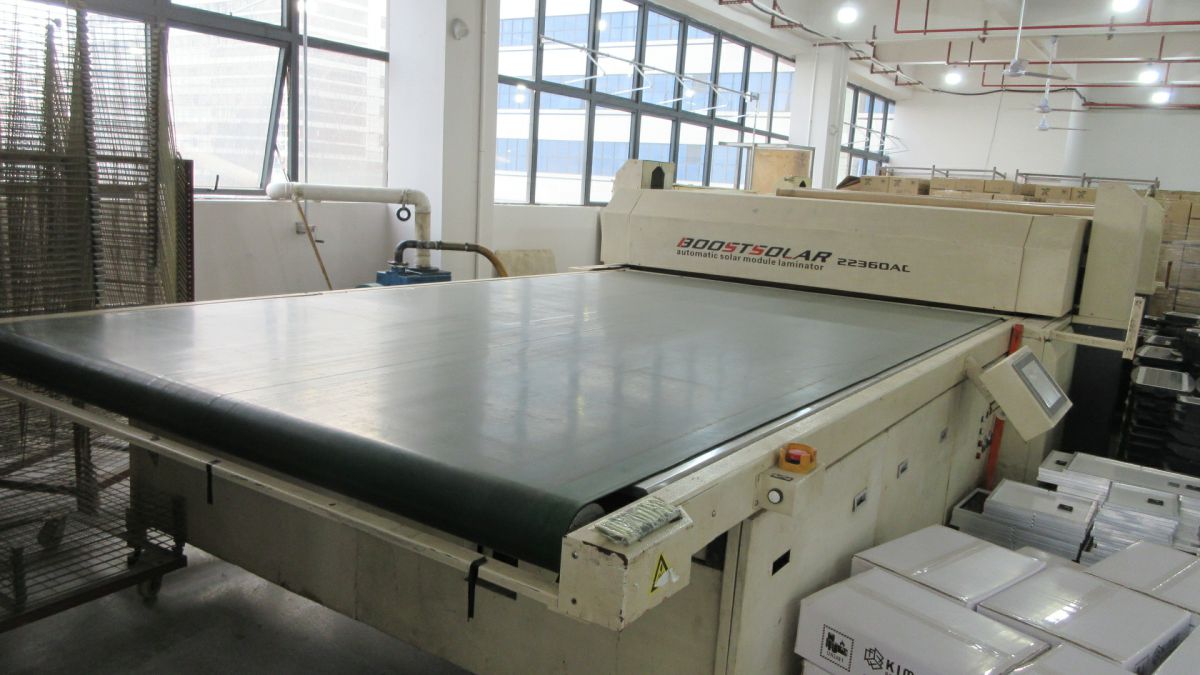
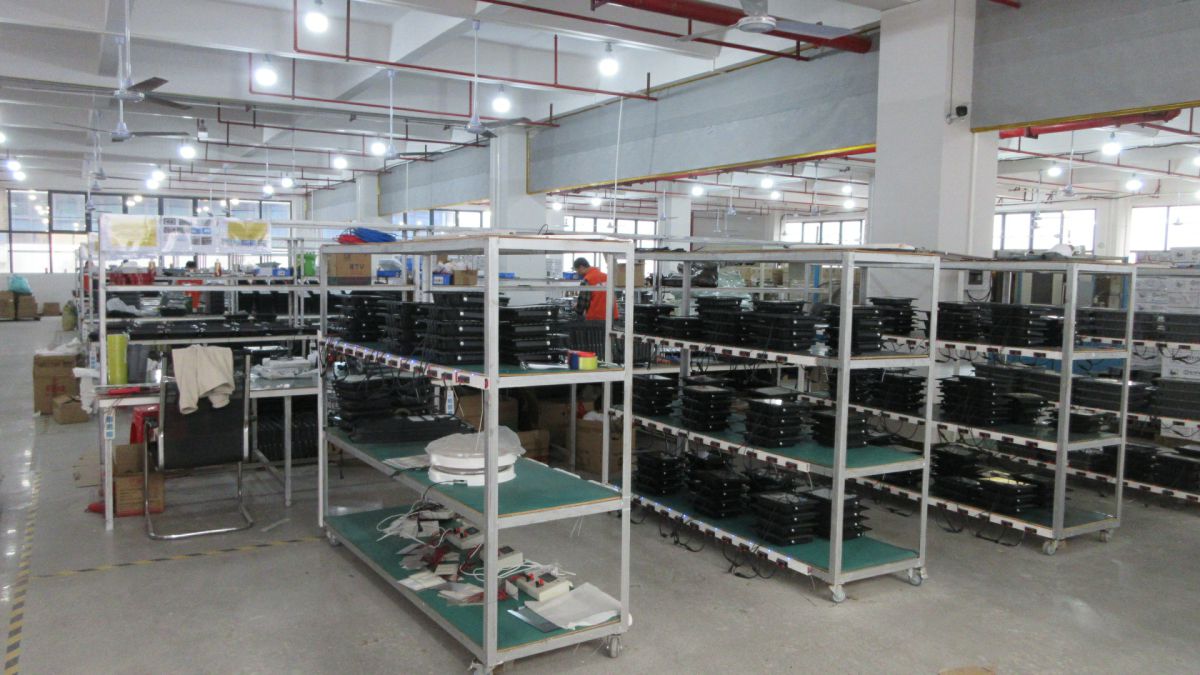
We maintain a well-stocked inventory of raw materials, ensuring stable supply, faster production cycles, and reduced lead times. This also helps us guarantee consistent product quality from the very beginning of the manufacturing process.
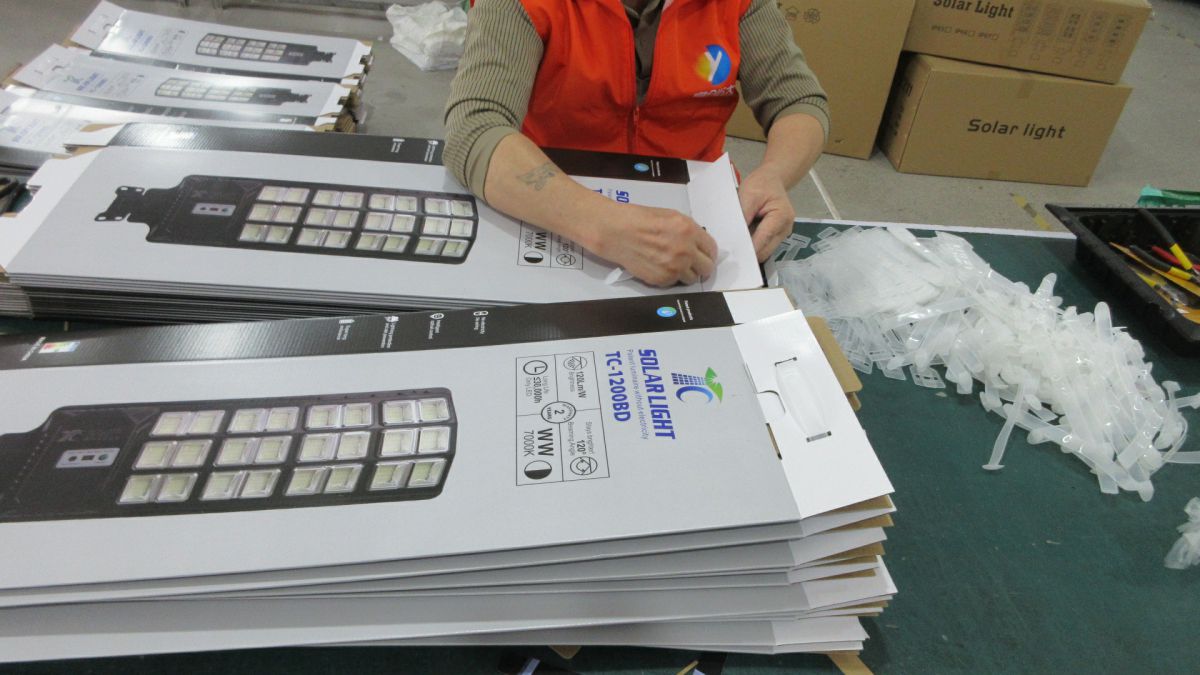
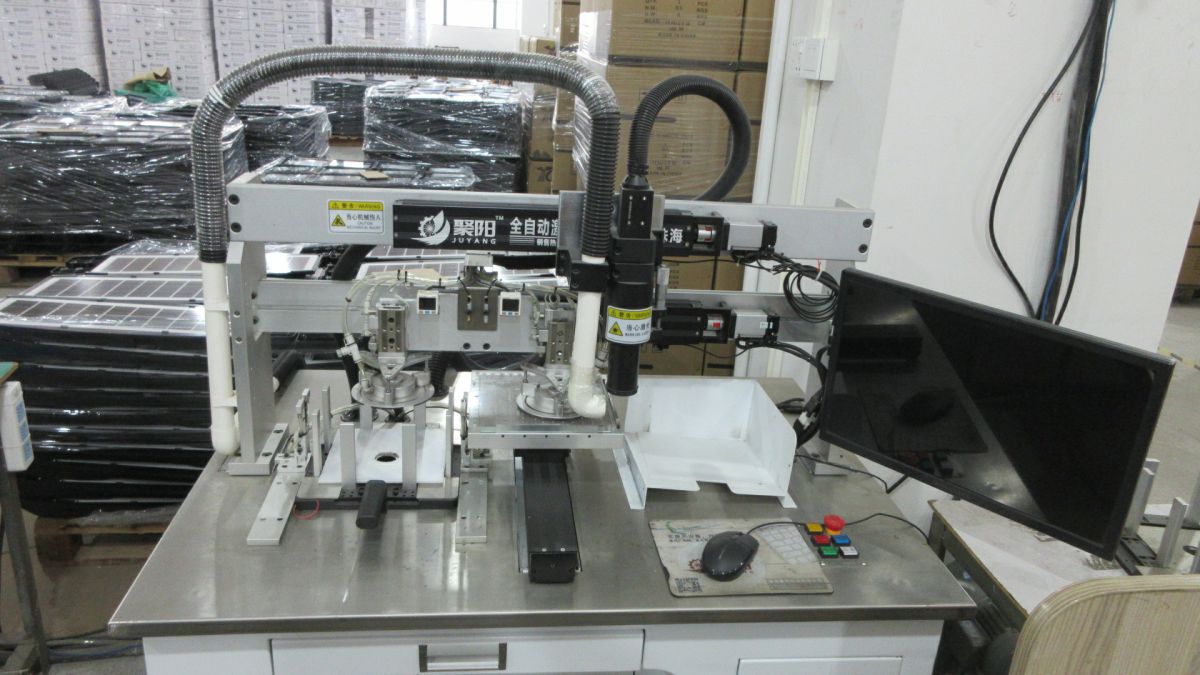
Our quality control manager has over 15 years of experience in lighting inspection and testing. We implement strict QC procedures across materials, production processes, finished products, and shipment stages. Any after-sales feedback is handled quickly, with root-cause analysis and effective corrective solutions.
We respond to customer inquiries and complaints within 24 hours and provide practical solutions within 48 hours, ensuring smooth communication and ultimate customer satisfaction.
We consistently invest in product innovation, smart lighting development, and energy-saving technologies. Our goal is to expand our global presence and become a trusted long-term partner in the international lighting industry.
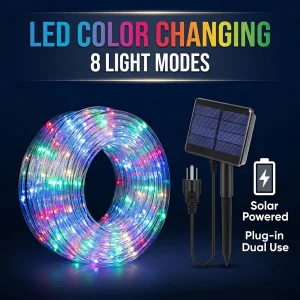
Explore our high-mast floodlights, explosion-proof canopy fixtures, and solar street lighting ranges.

Technical & commercial insights for international procurement managers and electrical contractors.
 Habel Lighting